Every month I get the same type of request: 'Find the cheapest part.' It doesn't matter whether it's a filter cartridge, a gearbox, or a small linear bearing. If you've ever had to justify a purchase to a plant manager, you know the pressure. But after managing a roughly $1.5M annual component spend for six years, I've learned that the cheapest purchase order often turns into the most expensive repair order.
So this is not a one-size-fits-all guide. There isn't one universal answer to 'which hydraulic filter, gear reducer, stepper, or bearing should I buy?' There are, honestly, three common scenarios. Let's walk through them.
Scenario A: You're building a new electric-driven machine
If you are designing a compact pick-and-place machine or retrofitting a small workstation, your main question is usually speed, precision, and budget. For most of these, a closed loop stepper motor is a very good compromise. It gives you closed-loop feedback (basically an encoder watching the motor) without the cost of a full servo system. In Q1 2025, I quoted two projects with closed loop stepper kits, and the savings versus comparable servos were still significant even with the encoder and driver added.
Pair that with a worm gear reducer when you need high reduction in a small package or a 90-degree output. Worm reducers are not the most efficient option on the market, though. If your machine runs continuously, the efficiency loss can cost you more in electricity than the reducer itself costs to buy. For intermittent duty, it's often totally worthwhile.
For the linear part, someone types 'what size is LM8LUU linear bearing' into the search box. The answer is simple: 8 mm bore, 15 mm outer diameter, 35 mm length. It is the long version of the LM8UU, so it has more contact area and usually smoother travel. That extra length matters if your shaft is supported and your load is light to moderate. I keep a small stock of LM8LUU bearings in the office; they are cheap, and it beats waiting three days for a single bearing when a prototype has to ship.
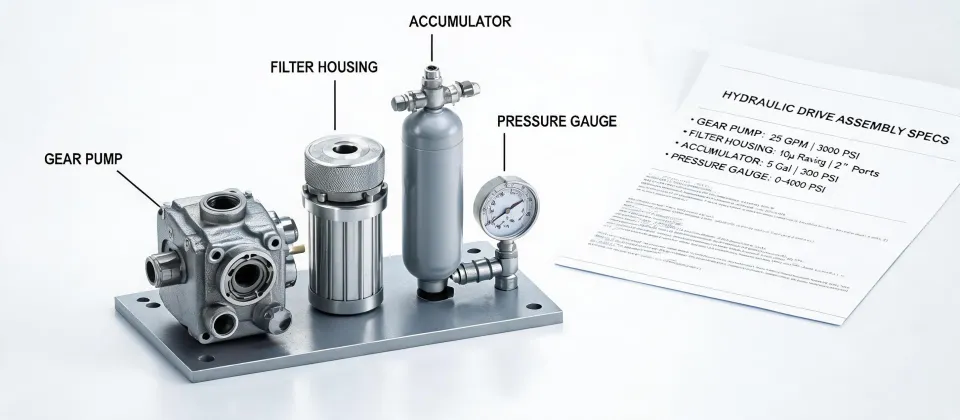
Do you need HYDAC parts in this scenario? Only if the machine has hydraulics. For an all-electric machine, skip it. But if there is a small hydraulic clamping unit, don't save $40 by buying a no-name filter element. Hydraulic filters are safety components as much as maintenance parts. A micron rating that is 'kind of close' is not close enough.
Scenario B: You're maintaining an existing hydraulic system
If you have a machine with hydraulic pumps, valves, and filters, the HYDAC official homepage is your starting point. I know it's not the flashiest site, but it has the PDF catalogs and part number details you need. According to the HYDAC official homepage (hydac.com, accessed February 2025), the product line includes filtration, pump, valve, and accumulator technology. I use that page to verify part numbers before I call a distributor.
From the outside, a replacement filter looks exactly like the original. The reality is that different filter media have different collapse pressures and contamination holding capacities. A cheap cross-reference may fit the housing but perform much worse. I've seen this cause erratic valve movement in a press line. It took two service calls to find it. The labor cost was more than ten times the difference in filter prices. To be fair, some cross-reference filters are fine. But you need the engineering data to know which ones.
What about worm gear reducers in a hydraulic plant? They show up on feeder conveyors, mixers, and auxiliary drives. If yours drives a load with occasional reversal, a worm gear reducer can be a good choice because of its high ratio and self-locking tendency. But don't downsize based on a claimed 'average' load. Check the service factor. In Q2 2024, I compared three quotes for a 2.2 kW worm reducer. The lowest quote looked fine on paper, but the thermal limit was too low for the installation. I skipped it. Four months later, the plant needed a different component, and that original low quote would have been a heat-related failure waiting to happen.
Scenario C: You're retrofitting a line for closed-loop position control
Retrofits are where I see the most over-spending and under-spending at the same time. Some teams buy a full servo system because they think it's the only way to get closed-loop control. Others buy the cheapest open-loop stepper and are confused when missed steps cause scrap. The middle path is usually a closed loop stepper motor.
For a retrofit, define the moving mass, required acceleration, and cycle time first. If the load is light and the cycle time is not crazy, a closed loop stepper motor with an encoder will do the job. If you have vertical loads, add a worm gear reducer. The reducer reduces the reflected inertia mismatch and helps hold the load when power is off, assuming your worm gear reducer has the right lead angle. That is a detail you can confirm with the manufacturer.
You also need linear bearings. If you are replacing old guide shafts, check the shaft hardness before you order LM8LUU bearings. A standard linear bearing expects a shaft hardness around 60 HRC. If the existing shaft is softer, the bearings will wear early no matter which brand you choose. That's an easy cost trap to avoid.
How to tell which scenario you're in
Ask yourself three questions:
- Is the machine mostly electric, hydraulic, or a mix?
- Are you building something new, maintaining an existing system, or retrofitting old equipment?
- What is the duty cycle? Intermittent, continuous, or heavy shock loads?
If you are mostly electric and building new, start with closed loop stepper motors, worm gear reducers, and LM8LUU linear bearings. Use HYDAC only for the hydraulic ancillaries that exist on the machine.
If you are maintaining hydraulics, go to the HYDAC official homepage, find the exact part number, and then compare price and lead time. The official catalog gives you the engineering data you need to judge aftermarket parts.
If you are retrofitting, start with the motion profile, then check the mechanical drivetrain, and then decide whether you need a servo or a closed loop stepper. Don't choose the motor before you know the load and duty cycle.
One caveat: my experience is based on about 200 purchase orders for a 50-person automation company. If you are working with mobile excavators, presses with high-pressure hydraulics, or long-run production lines, your numbers and risk points will be different. Talk to a local HYDAC distributor for hydraulic-specific advice, and verify bearing and reducer specs against your actual loads.
At the end of the day, efficiency is a competitive advantage. But efficiency doesn't mean 'cheapest part.' It means getting the right component the first time, with the least downtime, and no hidden follow-up cost. That's the cheapest thing I've found in six years of buying.