In March 2024, I got a call at 4 PM from a maintenance manager whose production line was dark. The servo motor that drives the main conveyor had failed hours earlier, and the replacement he'd ordered from a discount listing had arrived that morning — with a mounting flange that didn't match anything in his plant. The wrong part was sitting in a toolbox. The right one hadn't been ordered yet. His customer's delivery truck was pulling in at 7 AM the next day.
You'd think someone who coordinates emergency parts for a living would tell you this story ends with a lesson about speed. It doesn't. I've handled 200+ rush orders in eight years, including same-day turnarounds for food and beverage plants where downtime is the most expensive problem you'll face all year. And the pattern is always the same: the real problem isn't how fast you can get a part. It's everything that happens between the line stopping and the phone call to someone who can help.
The surface problem: "I need it yesterday"
When production stops, everyone understands one thing: time. The maintenance team wants the line running. Sales wants the customer's order shipped. Management wants the cost center closed. So the immediate request is always the same — "get us a replacement as fast as possible."
That's a fair instinct. It's also where the trouble starts. Because panic narrows your decision-making to one variable, and that variable is usually the wrong thing to optimize.
In my experience, the rush leads to three shortcuts. They each look rational at the moment. They each end up costing more than the emergency they were meant to solve.
Shortcut #1: ordering what you can name, not what you have
The maintenance manager I mentioned was sure a stepper motor had failed. The replacement he bought was a stepper motor. But what was actually bolted to his conveyor was a servo motor. From three feet away, they look similar. Both drive motion. Both sit in the same frame size, roughly.
One is not the other.
Stepper motors run on open-loop control — they move in fixed increments and don't need feedback to track position. Servo motors use closed-loop feedback: an encoder or resolver tells the drive exactly where the shaft is at all times, which means higher torque at speed and tighter position accuracy. They're designed for different jobs, and they cannot be swapped without changing the drive, the wiring, and the control logic.
Why does this matter in an emergency? Because when "what's a stepper motor?" becomes a question you're answering after a failure — instead of before — you're already deep into the expensive part of the lesson.
In that same conversation, I asked whether they'd considered repair instead of replacement. The old motor had already been thrown out, so the option was gone. But it should have been raised earlier: a servo motor repair — replacing the bearings, encoder, or winding set — can be genuinely faster and cheaper than sourcing new. Only if you catch it early. The moment they bought the wrong replacement, that door closed.
Shortcut #2: "will fit" is not "will last"
Last spring, my team sourced a set of straight bevel gears for a packaging line. The customer had found a cheaper set online, and the dimensions matched perfectly: same tooth count, same bore, same overall size. It went on smoothly. For six weeks, the machine ran better than it had in years.
Then a tooth chipped.
The problem wasn't geometry. It was metallurgy. Straight bevel gears transmit power across intersecting axes, with load carried along the tooth face. That means material grade, case hardening depth, and tooth profile quality matter as much as tooth count. A gear that looks identical in the catalog can have a far lower load rating if it's made of a softer material or machined to looser tolerances.
I had a day to decide on that gear set. Normally, I'd ask for the original spec sheet: module, pressure angle, material, hardness, dynamic load rating. But there was no time, and the customer needed a decision. I let the price and the dimensions do the talking. That's on me.
We paid for it in round two: a second shutdown, another visit from the repair crew, and a premium-freight order for the correct part. The customer's $400 savings turned into a $6,400 bill.
The deeper cost of "good enough"
Let's put the real number on the table. In food and beverage processing, unplanned downtime can run $10,000 to $50,000 per hour depending on the line. Add in wasted product, missed delivery windows, and overnight overtime labor, and the part itself becomes a rounding error.
So why do we keep making decisions based on the part price?
Because it's the only number we know in the moment. The cost of a second failure is abstract. The savings on this invoice is concrete. That's a trap.
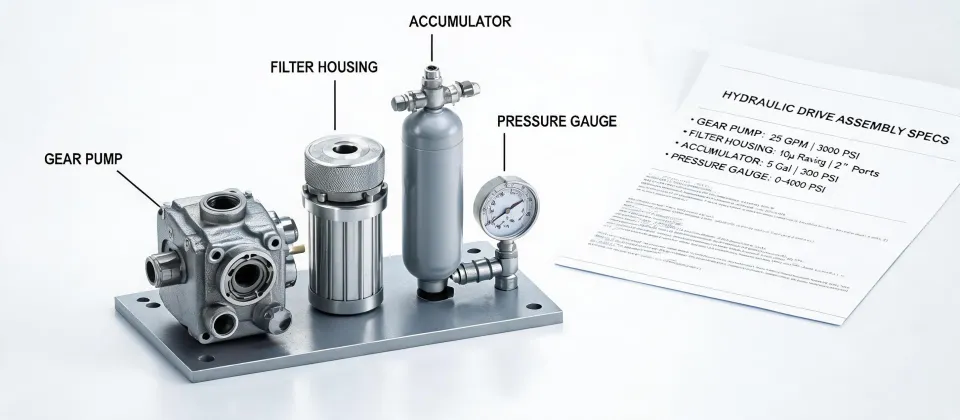
This is also where the "genuine parts" conversation gets real. You'll see listings for "hydac industrial parts" all over the internet — authorized distributors, resellers, and some sources that are harder to verify. A lookalike filter cartridge might thread on fine, but its filtration rating may not meet the original spec. In a hydraulic system, that difference shows up in a contamination analysis, not in a visual inspection.
According to ISO 4406, fluid cleanliness is measured by particle count at three size thresholds. If a replacement filter doesn't meet the cleanliness target the system was designed for, every component downstream — pumps, valves, actuators — wears faster. Save $120 on a filter, and it can cost you $3,000 on a pump. My job, in an emergency, is helping people avoid that trade.
When we source a HYDAC component under pressure, we go through the authorized distributor network referenced on the HYDAC official homepage. That's not dramatic. It's risk management. You're not paying extra for the part — you're paying for evidence: the part number is real, traceability is intact, and the quality standard is verified.
Of course, that's my context. I can only speak to industrial processing environments, where a failed component can take a quarter-million-dollar machine down with it. If you're in consumer electronics with commodity parts, the math is different. But in hydraulics and drive components, "good enough" is rarely good enough.
What actually works when the line goes down
The fix for this problem isn't exotic. It's boring. And that's exactly why it works.
- Confirm what's actually broken. Get the nameplate photo, the part number, and a description of the failure mode. Is the motor drawing current but not turning? Does the controller report an encoder fault? Ten minutes of confirmation prevents 36 hours of re-shipping.
- Ask the repair question before the replacement question. Servo motor repair can be a legitimate option — bearings, encoders, and connectors fail far more often than the motor's core. A proper diagnosis might have that line running in 24 hours instead of four days.
- Source from verified channels. For HYDAC parts, that's the distributor network listed on the official site. For gears, that means a manufacturer who can supply material certificates and test reports. You're not paying a premium — you're buying certainty.
- Match the full spec, not the silhouette. Straight bevel gears need module, tooth count, pressure angle, material, and hardness. Motors need voltage, torque, speed, and feedback type. "It looks right" is not a specification.
- Do the homework before the crisis. Build a shortlist of verified vendors for your critical components and keep it in a shared file. When the line stops, you don't want to be googling at 4 PM.
Bottom line
The fastest option is rarely the right option. The answer is to spend a few minutes slowing down — confirming the part, the spec, and the source — and then rush everything else. It sounds counterintuitive. It's also the difference between a one-day outage and a two-week saga.
So glad we built our vendor verification list before the next big failure. We almost didn't. A few years ago, I approved a quote from an unverified supplier because the CEO was waiting and the line was down. I had two hours to decide. In hindsight, I should have pushed back. But I made the call with incomplete information, and we paid for it with a repeated failure a month later.
That's the thing about emergencies: they punish people who skip the basics. And they reward people who hold their nerve. When the line stops, be the latter.