I manage quality compliance for an industrial equipment manufacturer. Every year I review about 200 unique components before they go into machines. In 2024, I rejected 12% of first deliveries for spec deviations—some small, one expensive. So when someone asks me whether to use a hydraulic or electric linear actuator, I don't start with marketing. I start with failure modes. Specifically, what happens when a linear actuator fails in your exact duty cycle.
What has changed is the answer. Five years ago, I would have defaulted to hydraulic for anything above 5 kN. Now, since 2020, electric actuators have closed a lot of the gap. The fundamentals haven't changed—hydraulics still gives you force density that electric motors struggle to match—but the execution around both options has transformed. Let me walk you through the comparison the way I actually review components.
What Happens When a Linear Actuator Fails? Hydraulic vs. Electric
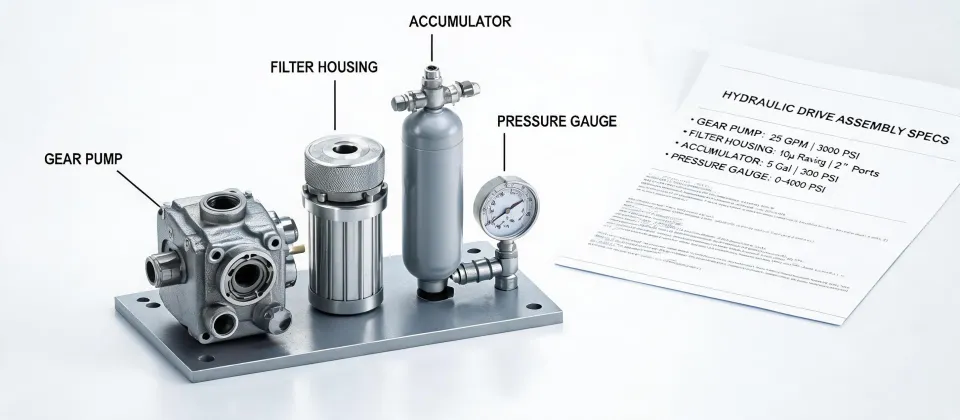
A linear actuator, in both worlds, converts rotary energy into linear motion. In a hydraulic system, that usually means a gear pump pushing fluid through a directional valve into a cylinder. In an electric system, it means a servo or stepper motor driving a ball screw or lead screw. The failure modes are not the same.
The most frustrating part of this comparison is that people ask 'which is better' when the real question is 'which failure mode can you tolerate?'
Hydraulic failure modes
Hydraulic actuator failures—or rather, the system failures that stop the actuator—are rarely caused by the cylinder itself. The root cause is almost always contamination or a worn pump. A HYDAC gear pump is fairly tolerant of fluid contamination compared to a piston pump, but the valve spools and cylinder seals are not. I've seen a cracked return-line filter housing let particles circulate for weeks. The actuator still moved, but the valve started sticking, and the cylinder seal began leaking. What I mean is, the actuator was the victim, not the source.
The other common failure is cavitation. If the pump inlet is restricted or the fluid viscosity is too high, the pump gets noisy and the actuator moves erratically before it stops altogether. This is one reason I treat pressure-relief and filtration as part of the spec, not an upsell. According to ISO 4413, hydraulic systems need overpressure protection. I'd add that they need contamination control too. (Source: ISO 4413:2010)
Electric failure modes
Electric actuators fail differently. The most common issues I see are thermal overload, lost steps, screw wear, and cable flex failures. With a closed-loop servo, the drive will usually detect a fault and stop the machine. With a stepper, the failure can be silent. Look at any stepper motor diagram: rotor teeth, coil windings, and permanent magnets. If torque demand exceeds holding torque, the rotor just falls out of sync with the drive pulses. No feedback, no alarm—the actuator simply ends up in the wrong position.
That's probably the most dangerous failure mode in this whole comparison. A hydraulic leak is visible. A stepper lost-step is invisible.
For industrial motors, IEC 60034-1 defines duty types. An actuator rated S2 is for short-time duty only. If your machine runs it all day, you're already designing for failure. (Source: IEC 60034-1)
Control Precision and Repeatability
Hydraulic actuators can be precise, but not without a proportional or servo valve. A standard on/off directional valve will give you end positions and not much else. Add a proportional valve and a position sensor, and you can repeat positions to perhaps ±0.1 mm. That's acceptable for many presses and clamps. It's not impressive by electric standards.
Electric actuators have an inherent advantage here. A servomotor with an encoder holds position tightly. A hybrid stepper with microstepping can also do good things—though not as good as a servo. To understand why, look at a stepper motor diagram and count the rotor teeth: a typical hybrid stepper has 200 full steps per revolution. Microstepping divides those steps electronically, but it doesn't guarantee absolute position. For absolute positioning, you need a closed-loop stepper or a servo.
One thing that still surprises some buyers: the small 'sg90 servo motor' you see in hobby kits is not a scaled-down industrial servo. I've reviewed proposals where someone specified an sg90 servo motor for a light positioning axis because the torque seemed enough. It wasn't. The sg90 is designed for radio-control models, not continuous industrial duty. It has a plastic gear train, a small DC motor, and no encoder. It will likely eventually drift or strip gears.
Maintenance and Diagnostics: Oil vs. Data
Hydraulic systems need discipline. Oil sampling, filter changes, seal inspections. In my last Q1 audit, I rejected a power unit because the return-line filter was undersized for the pump flow. The vendor argued it was 'within industry standard.' Industry standard, in this case, meant cheaper. We rejected the batch and made them redo it. Since then, every contract in our department includes a filter sizing line item.
Electric systems need less fluid maintenance but more attention to mechanical parts. Ball screws wear, couplings loosen, cables flex. The upside is diagnostics. A servo drive will tell you torque, temperature, and position error. A hydraulic system won't tell you anything unless you add pressure sensors and condition monitoring. That data advantage is real, and it changes how you troubleshoot.
Even after choosing electric actuators for a packaging line in 2024, I kept second-guessing. What if the ball screws wore faster than the vendor promised? The commissioning weeks were stressful. It wasn't until the drive logs showed consistent torque values that I relaxed.
There is a certain satisfaction in watching a machine recover after a proper root-cause fix. The best fix I ever implemented was adding a HYDAC pressure filter before a proportional valve. That eliminated a recurring actuator seizure problem that had cost us two production shifts.
Sourcing and Documentation: HYDAC Catalog PDF vs. Motor Software
Documentation is a quality inspector's lifeline. On the hydraulic side, I keep a copy of the HYDAC catalog pdf on my desktop. I'm not being paid to say that; it's simply one of the few catalogs that lists pump displacements, pressure ratings, filter specs, and recommended cleanliness levels side by side. If you search for 'hydac catalog pdf', you'll get a technical document, not a brochure. That makes it easier to write an accurate purchase spec.
On the electric side, sourcing is less centralized. For motors and drives, I often have to collect data sheets, configuration software outputs, and CAD files from several different pages. That's not a flaw in the technology—it's just more fragmented.
According to ISO 4406:2017, cleanliness codes follow a three-number format based on particle sizes. A gear-pump circuit might tolerate something like 22/18/13; a servo-valve circuit would need much cleaner oil. That's why filter selection has to be part of the actuator spec, and why a good catalog helps. (Source: ISO 4406:2017)
So Which Should You Choose?
I can't give you a simple 'hydraulic wins' or 'electric wins' because it depends on the application. Here's how I frame it with our engineering team.
- Choose hydraulic when you need very high forces, shock loads, or a compact cylinder in a harsh environment. A HYDAC gear pump paired with a properly sized filter and a simple cylinder is a proven, robust route. The main condition: you need a maintenance culture that takes oil sampling seriously.
- Choose electric when you need precise positioning, clean operation, or quick reconfigurable motion profiles. A servomotor with a ball screw is ideal. A stepper can be acceptable for moderate loads if you include a home switch and perhaps an encoder for verification. Avoid the sg90 servo motor for anything beyond a lab prototype.
- Consider a hybrid: an electric motor driving a fixed hydraulic pump (electro-hydraulic actuator, or EHA). This is where the industry is evolving. You get the force density of hydraulics and some of the controllability of electrics. It's more expensive, but for certain axes it solves the 'which failure mode' trade-off.
And whatever you choose, spec the maintenance plan before you spec the actuator. I've rejected 12% of first deliveries in 2024, mostly because someone skipped a review step. The worst failures I see are not between hydraulic and electric—they are between 'we assumed it would work' and 'we actually verified it.'