-
Four Buying Situations, Four Different Answers
-
Situation 1: You're Still Proving the Concept
-
Situation 2: Production Equipment That Needs Adjustable Electric Speed
-
Situation 3: High Force and Harsh Conditions Point to Hydraulics
-
Situation 4: Constant-Speed Right-Angle Drives and Straight Bevel Gears
-
So Which Situation Are You In?
-
The Cost Side of the Decision
I'm a procurement manager at a mid-sized machinery builder. For the past seven years I've managed our motion-component budget, roughly $1.2 million per year, and I've negotiated with more than 40 vendors. That doesn't make me the smartest person in the room. It just means I've watched the same buying mistake happen more times than I can count: engineers start with a component name, then work backwards to justify it.
Last month we had three projects running at the same time: a hydraulic manifold redesign, a conveyor transfer with a badly worn right-angle drive, and a bench test for a new gripper. In one week I got three requests: one for the HYDAC cartridge valve catalog, one for a replacement pair of straight bevel gears, and one for an MG90S servo motor. Different motion technologies, different contexts. That's not unusual in this industry, and it's exactly why there's no universal answer to the question of which component is best. The right question is: best for what kind of machine, under what kind of duty?
Here's the framework I've used to keep us from over-specifying and overspending. It won't give you one perfect part number, because that part number doesn't exist until you know your operating conditions.
Four Buying Situations, Four Different Answers
In my experience, most motion-component searches fall into four buckets:
- You're still proving a concept on the bench, where an MG90S-class servo might actually be acceptable.
- You need adjustable speed from an electric motor in production, which brings up VFD compatibility.
- You need high force in a compact, dirty, or shock-loaded space, which points toward hydraulics and HYDAC industrial parts.
- You need continuous power transfer at a right angle and roughly constant speed, which is classic straight bevel gear territory.
None of these is better than the others. They're just different answers to different problems.
Situation 1: You're Still Proving the Concept
An MG90S servo motor is a hobby-class micro servo, not an industrial actuator. It's usually around 9 grams, has metal output gears, runs at 4.8 to 6 volts, and produces roughly 1.8 kg-cm of stall torque at 4.8 volts. It responds to a 50 Hz PWM position signal. It does not come with an encoder, a servo drive, or a duty-cycle rating for 24/7 factory use. For a production machine, I won't specify it. For a bench fixture that moves a lightweight link arm at low load, it does exactly what you need, and it's cheap to replace.
Here's the counterintuitive recommendation: if the goal is to prove the mechanism works, don't buy an industrial servo yet. Spend the saved money on instrumentation instead. The mistake I've seen more often is the opposite: a team buys an industrial motor and drive at prototype stage, and then has no budget left to measure the forces that actually matter.
The risk comes later if someone treats hobby-class test data as if it applies to production. It doesn't. An MG90S can validate geometry, range of motion, and basic timing, but not wear, torque repeatability, or thermal behavior under a real production cycle. When you need that data, step up to a proper servo system.
One procurement note: don't let a supplier make you feel stupid for placing a small test order. I've bought $200 worth of prototype parts from companies that later became major suppliers. If a distributor treats a $300 order like a nuisance, that tells you something before you hand them a $30,000 production order.
Situation 2: Production Equipment That Needs Adjustable Electric Speed
This is where the question what motors are compatible with vfd usually comes from. The short answer: a standard VFD is designed to run a three-phase AC induction motor. It changes the voltage and frequency supplied to the motor, which changes its speed. That sounds simple, but the output waveform from a VFD is not a clean sine wave. It's pulse-width modulated, and those fast voltage pulses can stress motor insulation over time.
Per NEMA MG 1 Part 31, a motor used on an adjustable-speed drive should be specified for inverter duty if you expect it to handle that environment reliably. That's an important distinction. A motor that happens to spin when connected to a VFD is not the same as a motor that is actually rated for it.
As of early 2025, most reputable three-phase motor manufacturers offer inverter-duty versions. The problem is that older motors, bargain-brand motors, and single-phase motors do not necessarily meet that standard. Here's what I check before approving a purchase:
- Is it a three-phase induction motor? If you have a single-phase motor, a standard VFD is usually not the right answer.
- Is it marked inverter duty or variable-speed rated? If not, the winding insulation may not survive continuous VFD operation, especially with long cable runs.
- What is the constant-torque speed range? Many TEFC motors lose cooling at low speed because their shaft-mounted fan slows down. If the machine runs at low speed for long periods, you may need a motor with forced ventilation or a wider constant-torque rating.
- How long is the cable between the drive and the motor? Long cables create reflected voltage spikes. Sometimes you need a reactor or a dV/dt filter at the drive output.
I've seen the low-price path go wrong here. A standard motor and a cheap VFD can look like a bargain on paper. Then the motor fails after a year of low-speed operation, and the total cost is far higher than buying the right inverter-duty motor upfront. When I compare quotes, I ask the vendor to confirm in writing that the motor is suitable for the speed range and cable length in the specification. That one sentence has saved us more than once.
Situation 3: High Force and Harsh Conditions Point to Hydraulics
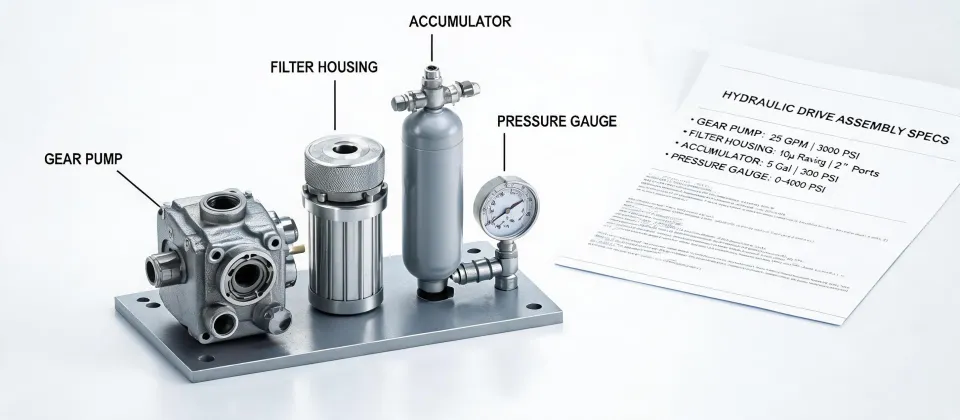
Electric drives have improved a lot, but they still can't match the raw force density of hydraulics in a compact envelope, especially when the environment is dirty, wet, or subject to heavy shock loads. When that's your situation, HYDAC often shows up on the radar. HYDAC industrial parts include filter elements, gear pumps, accumulators, and cartridge valves, and they're commonly found on machines that need reliable fluid power.
The HYDAC cartridge valve catalog is a useful starting point, but it can be deceptive. Cartridge valves are installed directly into a machined manifold, which removes external hoses and leak points. The simplicity is real, but the selection requires attention to flow rating, pressure rating, spring range, and pilot characteristics. Two cartridges can have the same thread and the same external dimensions and behave completely differently inside the manifold.
I made that assumption once. I assumed same dimensions meant same performance, and it didn't. The valve looked identical to the original, but the cracking pressure was different, and a cylinder crept under load. That mistake cost us an afternoon of troubleshooting and a tank of hydraulic oil. Now I verify the part number and the specification, not the photo.
Filtration is the other thing I refuse to cheap out on. Hydraulic failures are often contamination failures, and target cleanliness levels like those defined in ISO 4406 exist for a reason. A filter element that costs a few dollars less than the HYDAC original can have different media, different bypass behavior, or different collapse rating. It may look fine in the box and then cause expensive damage later. In that context, a cross-reference number is a starting point, not a substitute for verifying the actual specification.
Situation 4: Constant-Speed Right-Angle Drives and Straight Bevel Gears
Sometimes the most cost-effective solution is also the most mechanical. If you need to transfer power at roughly constant speed and change the axis of rotation by 90 degrees, a bevel gearset can beat a motor-and-controller solution on total cost of ownership. This is where straight bevel gears still make sense.
Straight bevel gears are simpler and usually more economical than spiral bevel gears. They're appropriate for low-to-moderate speed applications like transfer drives, indexing conveyors, and auxiliary takeoff shafts. At high pitch-line speeds, they tend to be noisy and harsh compared to spiral bevel gears, which engage more gradually. So if the application is fast or heavily loaded, spiral bevel is often the better call. But for many slower continuous-duty applications, straight bevel gears are perfectly adequate.
The buying trap I've seen is purchasing a gear pair by tooth count alone. Straight bevel gear performance depends on material grade, case hardening depth, tooth profile, mounting distance, and backlash. If the contact pattern is wrong, the set wears fast no matter how good the steel looks.
I knew I should have asked for material certifications on one budget gear set, but I thought what are the odds? The odds caught up with me around eleven months later when the tooth flanks started spalling. Replacing the gearset was cheap. The disassembly, downtime, and lost production were not.
So Which Situation Are You In?
Here's a quick decision path I use when a request lands on my desk:
- Are you still proving whether the mechanism works at all? If yes, bench-test components such as an MG90S servo are acceptable for concept validation.
- Does the shaft speed need to change during normal production? If yes, look at a three-phase inverter-duty motor with a properly sized VFD.
- Is the core requirement very high force in a compact, dirty, or shock-loaded space? Then hydraulics, with components from HYDAC or a similar established manufacturer, is probably the right direction.
- Is the speed essentially constant and the main challenge simply changing the rotation axis by 90 degrees? Then start with a mechanical solution like straight bevel gears before adding electronics.
Real machines often cross these lines. One of our assembly systems uses HYDAC hydraulic clamps to hold a part, a VFD-driven spindle for machining, and a bevel gearbox for an auxiliary auxiliary shaft. Each choice was made for a different reason, and that's fine. The problem is never the technology mix. The problem is choosing a component before you understand the operating conditions.
The Cost Side of the Decision
From where I sit, total cost of ownership matters more than unit price. A cheaper motor that fails early is not cheaper. A filter that saves twelve dollars but lets contamination through is not cheaper. A gearset that requires an unscheduled shutdown a year later is definitely not cheaper.
When I compared quotes for a $4,200 annual filter contract recently, one supplier looked better on the base price. After I added freight and minimum order quantities, the other supplier was actually about 11 percent lower in total. That kind of difference is invisible if you only compare unit prices, so I always build a simple spreadsheet before approving a purchase. It takes fifteen minutes and it has saved us money more times than I can count.
One last thing: small orders are not bad orders. Many of you are reading this while trying to buy a single test servo or a small batch of hydraulic parts. I've been there. The suppliers who treated my early $200 orders with respect are the ones I still call today for larger production orders. Buying the right part, at the right specification, for the right stage of your project is what matters. Everything else is just noise.